Industrial Grade Lubrication — Industrial food-grade grease is formulated to withstand extreme temperatures and pressures. It provides superior lubrication for machinery in demanding environments, ensuring smooth operation and reduced wear.
Food Safety Compliance — This type of grease is designed for use in food processing and packaging applications. It meets strict regulatory standards for incidental food contact, ensuring product safety and preventing contamination.
Corrosion Protection — Industrial food-grade greases often contain additives that protect metal surfaces from rust and corrosion. This is crucial for maintaining the longevity of equipment exposed to moisture or harsh cleaning agents.
Water Resistance — Many industrial greases offer excellent resistance to water washout. This ensures that the lubricant stays in place and continues to protect components even in wet or humid conditions.
Extended Equipment Life — Proper lubrication with high-quality industrial grease reduces friction and wear on moving parts. This can significantly extend the operational lifespan of machinery and reduce the need for premature replacements.
Description
• Available in various sizes and brands to meet diverse industrial needs.
• Specifically formulated for food processing environments, ensuring safety and compliance.
• Suitable for lubricating machinery and equipment in food manufacturing plants.
• High-quality grease designed for optimal performance and equipment longevity.
• Offered in a range of types to suit different operational requirements.

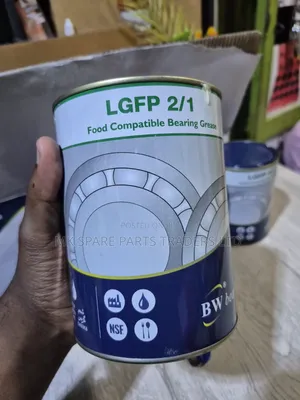 This itemIndustrial Food Grade Grease
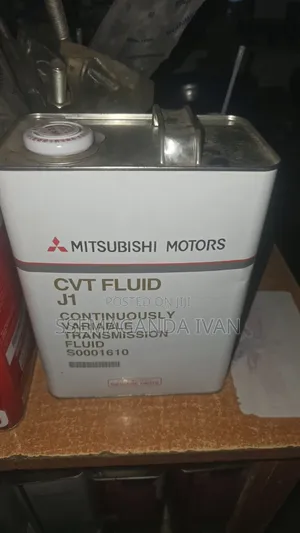 Brand New CVT Fluid for Mitsubishi Cars
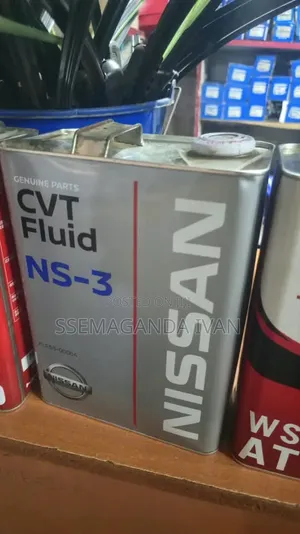 Brand New Nissan CVT Fluid NS-3 Transmission Oil


